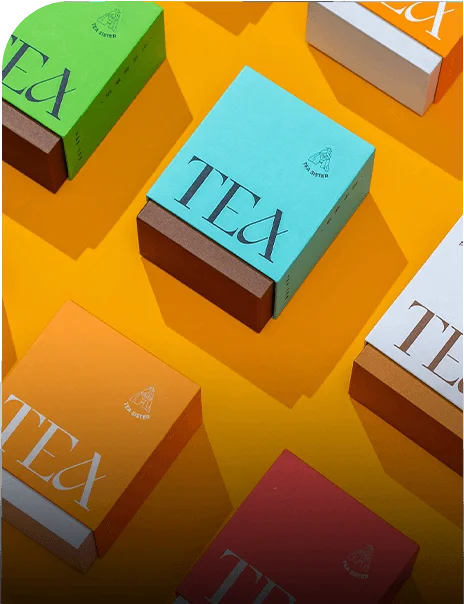






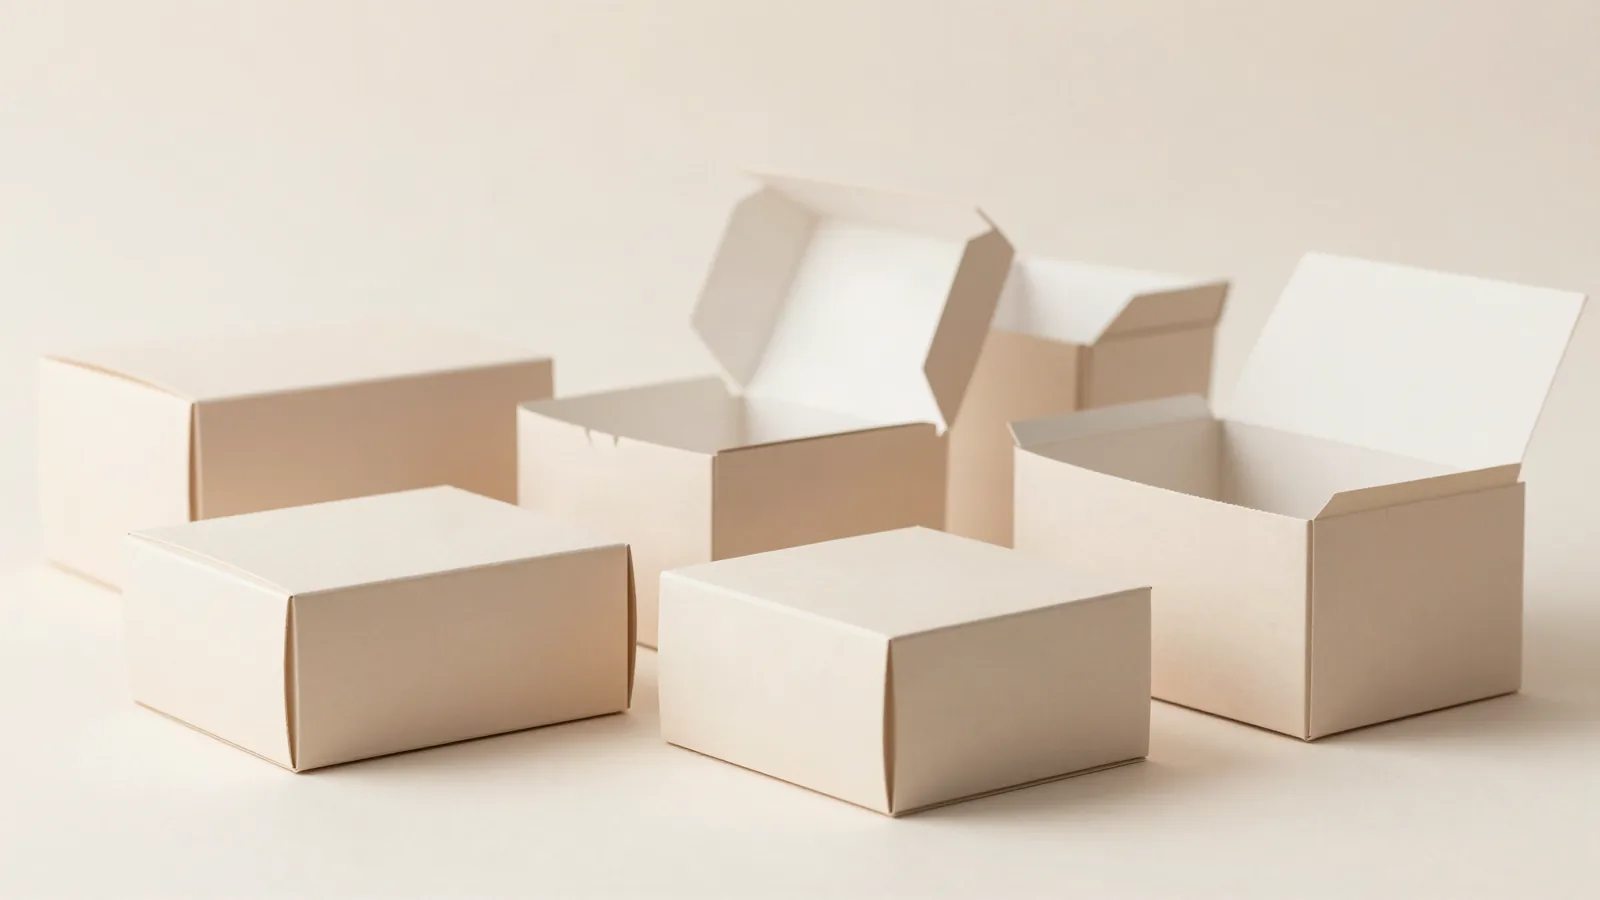


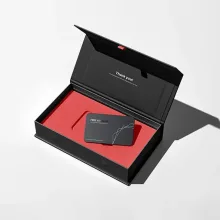


















A custom sliding box is a package with a moving tray, sleeve, lid, or base. The dieline is the flat cutting template that shows the cuts, folds, glue areas, and artwork zones before production. Start with the product in its finished wrap, then define the travel direction, stopping point, grip edge, clearance, and the way the box should look when partly open.
Sliding motion changes the specification. A tray can hold the product or an insert, while a sleeve controls the reveal and protects the tray when closed. That creates more interfaces than a simple folding carton. The physical movement deserves a test before the finish is approved.
What makes a sliding box different from a regular carton?
The opening path is the difference. A sliding box moves one component past another instead of lifting a lid or opening a tuck flap.
Mark the direction of travel, front panel, tray stop, grip area, sleeve mouth, and any point where the product or insert could catch. A sleeve that is too tight creates drag. Too much clearance lets the tray wander and can misalign the artwork. Check the closed, partly open, and fully open positions with the actual packed product.
Which sliding structure should I compare?
Each structure changes the reveal, the number of parts, and the fit checks required.
| Structure | Typical role | Buyer checkpoint |
|---|---|---|
| Drawer or slide | Tray moves through a sleeve | Pull force, tray stop, and clearance |
| Two-piece rigid | Separate lid and base | Lid fit, wall alignment, and reveal |
| Sleeve and tray | Printed outer wrap over an inner piece | Overlap and panel orientation |
| Magnetic flap | Hinged opening with repeat access | Closure alignment and artwork folds |
| Mailer | Parcel-led alternative | Roll end tuck top and packed footprint |
A drawer or slide suits a deliberate pull-out. A two-piece rigid box separates the lid reveal from the base. A sleeve and tray keep the outer component visually simple, while a magnetic flap changes the opening angle and front panel. A mailer is the parcel-led comparison. Test the assembled movement before adding an insert or finish.
How should I plan tray and sleeve clearance?
Measure the product in its final wrap, not the bare item. That measurement sets the tray cavity, insert walls, sleeve mouth, grip edge, and closed position.
Allow room for insertion and removal, but keep the tray from shifting inside the sleeve. Record the product contact points and any insert walls. An insert with too much empty space lets the product rattle, while an overly tight tray can scrape the sleeve or make the grip edge hard to use.
Which boards are common for sliding packages?
Folding-carton versions commonly use SBS, C1S, or C2S paperboard in the 12 to 24 pt range. Kraft board in the 18 to 24 pt range gives a natural surface. Here, pt means points, a board-thickness measure.
Rigid drawer boxes commonly use 1.5 to 3 mm chipboard wrapped in 100 to 157 gsm art paper. GSM means grams per square meter, a paper-weight measure. If the sliding presentation box travels inside a shipping outer, corrugated E, B, or C flutes can be considered, with 32 ECT as a common corrugated reference. E-flute is a thinner corrugated profile than B-flute and often carries finer print detail, while B-flute gives a thicker profile. ECT means edge crush test.
How should print and finish sit across moving panels?
Offset CMYK is common for detailed paperboard artwork, while digital printing can suit a short run or artwork variation. Matte or gloss lamination changes glare on the sleeve and tray. Soft-touch changes the hand feel. Spot UV, foil stamping, embossing, and debossing should stay on named panels and away from moving edges.
Mark folds, seams, sleeve overlap, tray edges, grip areas, and glue zones on the dieline. Keep fine type clear of scores. Check bleed and barcode quiet zones in the digital proof, especially where the sleeve covers the tray when closed. Low-resolution art and RGB files can change the result when they reach the selected press.
What dimensions should the sliding-box dieline show?
State length x width x depth, and label each value as inside or outside. Inside measurements control the tray cavity, insert position, and product clearance. Outside measurements control the assembled footprint.
About 1/16 in, or 1.5 mm, is a common industry tolerance, subject to the structure and material. The dieline should show cut lines, fold lines, glue areas, sleeve openings, tray stops, grip areas, artwork-safe zones, and separate rigid wrap components.
Which product examples help me compare the opening?
Custom votive candle boxes frame compact cavities and front-facing print. Custom undergarments boxes give a larger presentation reference where a tray, fold, or sleeve controls the reveal. Custom tuck top mailer boxes provide a parcel-oriented alternative when shipping matters more than drawer motion.
Use the examples to identify structural questions, then measure the actual contents. The catalog does not replace a product-specific cavity and movement check.
What should I send for a sliding-box quote?
- Finished product dimensions, wrap, insert, and tray position.
- Opening direction, sleeve travel, grip area, tray stop, and desired reveal.
- Board, rigid wrap, print coverage, finish, window, or insert requirements.
- Artwork status, folds, glue zones, seams, and moving edges.
- Delivery destination and whether the package is for display, gifting, shipping, or all three.
Custom Packaging Lane quotes sliding boxes from a 100-unit minimum, with pricing from $0.49 per unit at volume, quoted to spec. Production is typically 8 to 10 business days after proof approval, plus delivery. Free US shipping and free design support are available, and a free dieline is included in the setup. The $19.99 sample kit is credited toward the first order. Send the movement brief through custom packaging design.
Frequently Asked Questions
How does a sliding box open?
A sliding box moves a tray through a sleeve, or separates a lid and base along a defined path. The specification should show the travel direction, grip area, stopping point, and product position. Those details affect clearance and artwork, so check the assembled box with the real contents.
What clearance should a drawer tray have?
A drawer tray needs enough clearance for smooth insertion and removal, while the packed product needs enough support to avoid excessive movement. Specify the product wrap, insert, tray walls, sleeve mouth, and stop together. A physical sample reveals friction, looseness, or a grip edge that becomes difficult to use.
Which board references work for sliding boxes?
SBS, C1S, or C2S paperboard in the 12 to 24 pt range is a common folding-carton reference. Kraft board in the 18 to 24 pt range gives another surface direction. Rigid versions commonly use 1.5 to 3 mm chipboard wrapped in 100 to 157 gsm art paper. Choose around movement, stiffness, and finish.
How should artwork handle moving panels?
Artwork for a sliding box should keep the main message readable when the tray is closed and partly open. Mark sleeve overlap, tray edge, folds, seams, grip area, and insert windows on the dieline. Keep fine type away from moving edges and separate print, finish, cuts, folds, and glue layers.
Which catalog examples help compare sliding structures?
Votive candle boxes frame compact cavities and front panels. Undergarments boxes show how a larger presentation can use a sleeve, tray, or fold. Tuck top mailer boxes provide a parcel-oriented alternative. Use each product as a structural reference, then specify the actual dimensions, opening motion, and handling path.